étude de cas
Traceability of curved aerospace parts
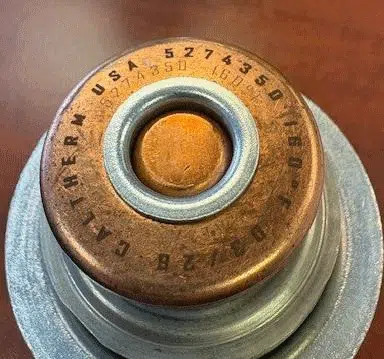
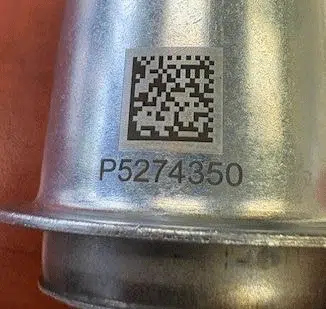
Permanent, readable identification of small cylindrical valve bodies, giving the aerospace manufacturer full in-plant and external traceability.
A 30W fibre laser to meet a 5-second cycle time
The 30W laser source was specified to achieve a cycle time of 5 seconds per part across stainless steel, brass and copper components.
Off-the-shelf rotary configuration, zero custom engineering
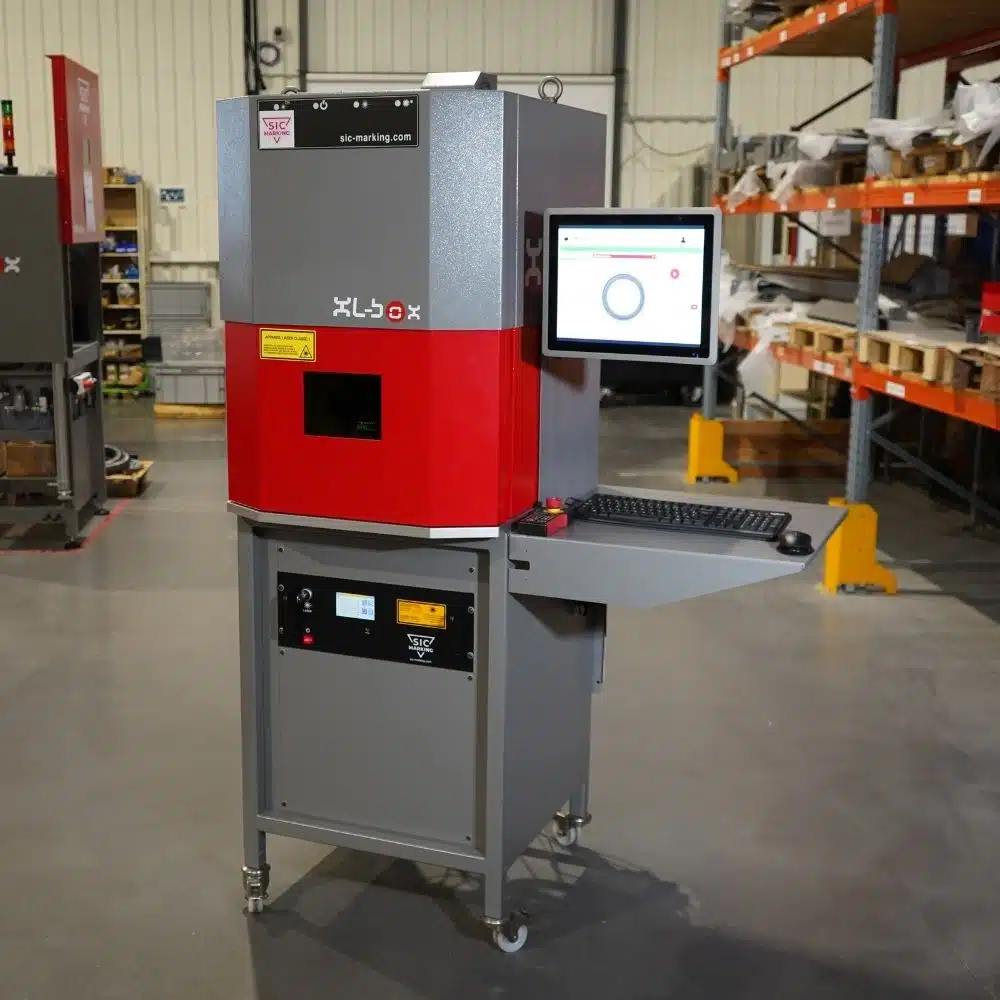
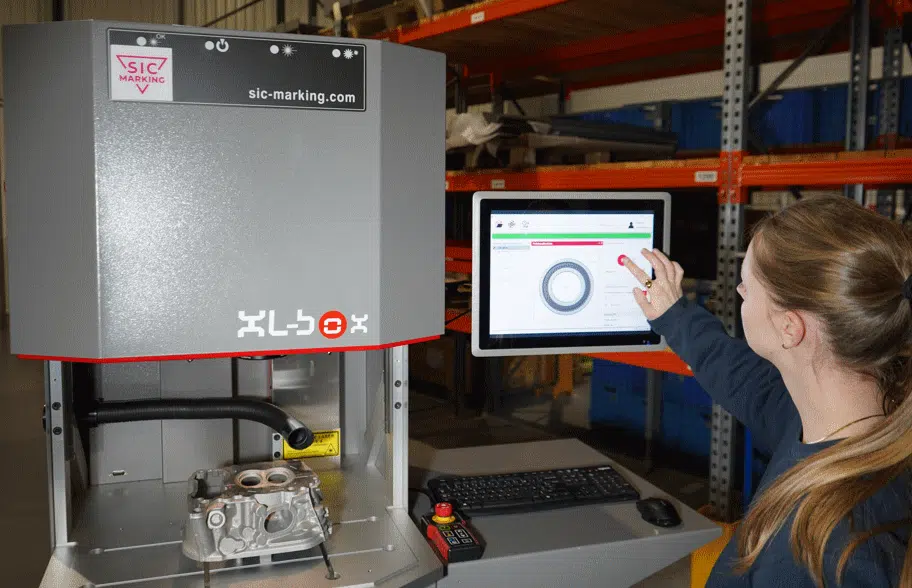
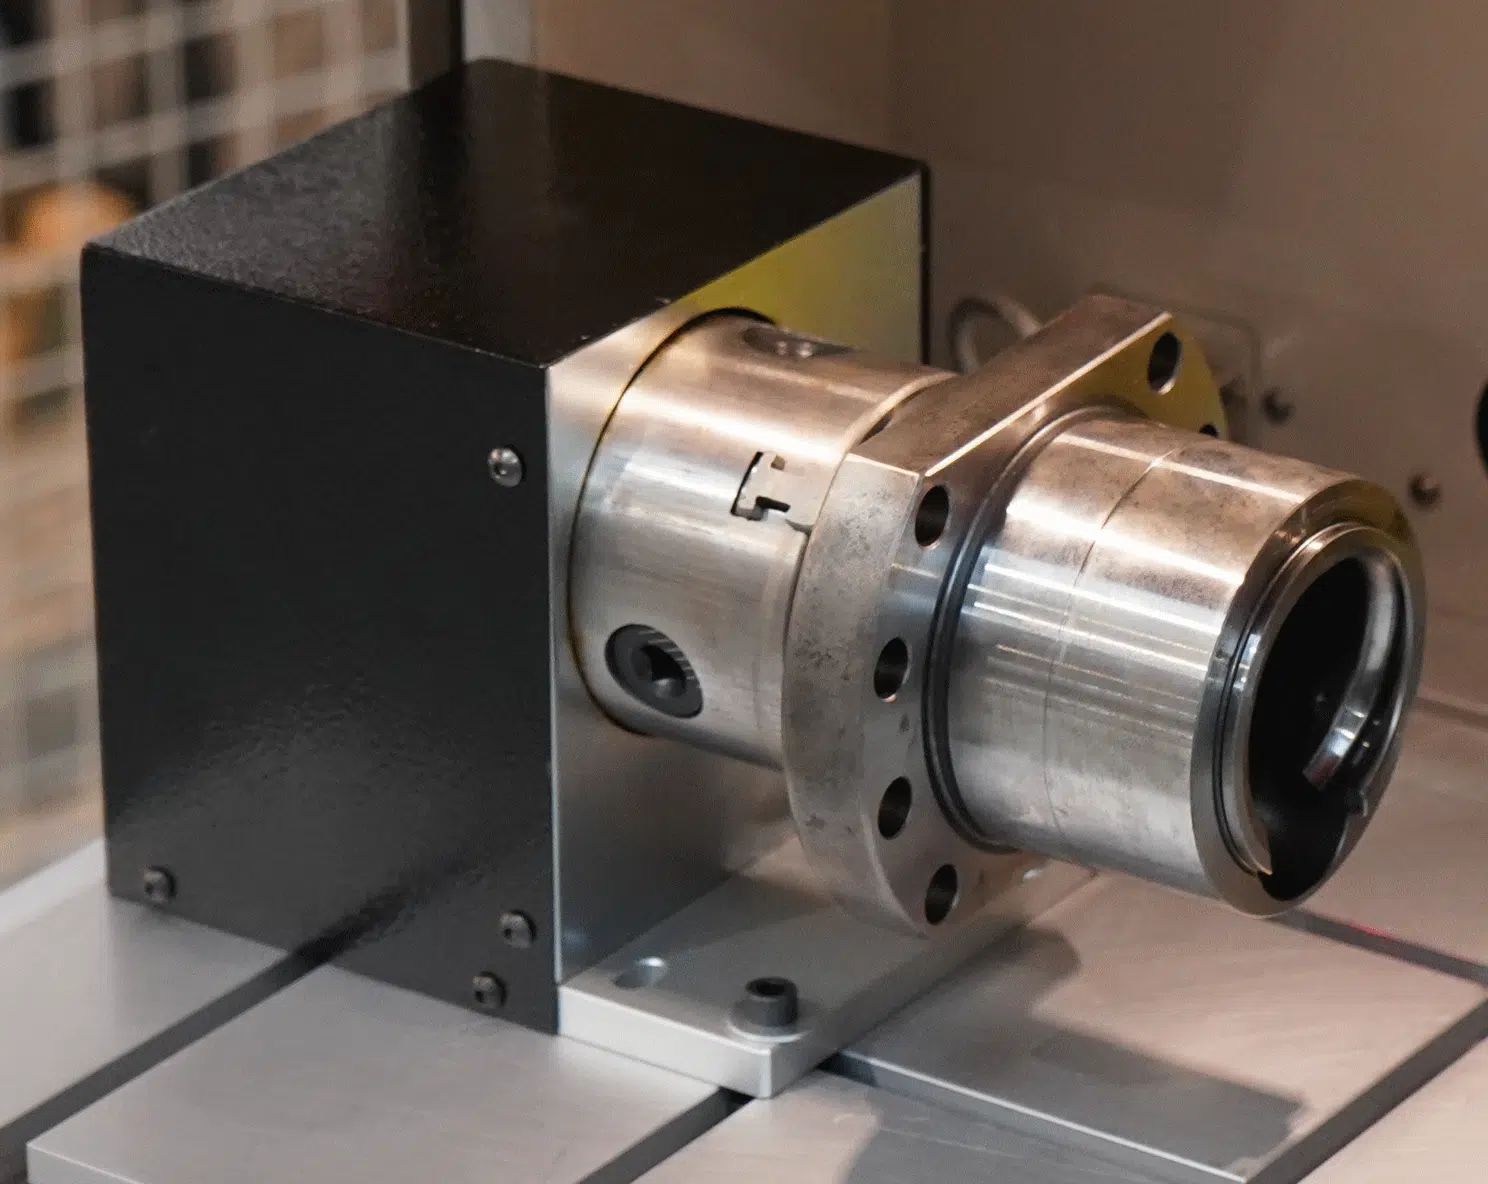
Equipped with a rotary axis, the XL Box EASY marks all the way around round parts, relying on a standard package made up of a chassis, a 254 mm lens and a fume extraction unit.
Target cycle time and mark quality achieved
The 5-second cycle time was met right from the initial production runs, and mark quality was compliant on each of the three materials.
The customer manufactures thermostatic pressure regulator valves used in aerospace thermal management systems. Each valve body requires a permanent, legible marking carrying the serial number, staging number, and company name. These markings serve both internal production traceability and external identification throughout the part’s service life, including the ability to trace manufacturing defects back to specific production runs.
The previous marking process could not keep pace with the required throughput. The production setup runs across three shifts with a single operator per shift, in a clean manufacturing environment. Any marking solution had to deliver consistent results at a rate of 5 seconds per part without adding complexity to the operator’s workflow.
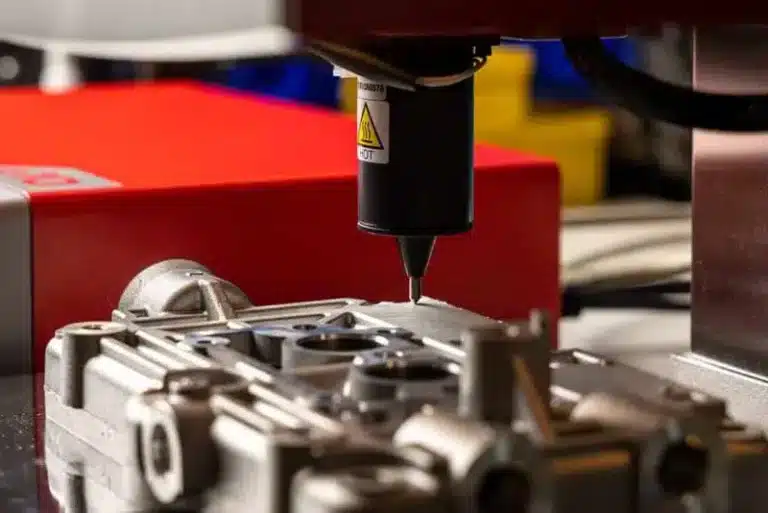
The core difficulty was geometric: valve bodies are small, round parts with curved outer surfaces. Achieving a clean, readable mark on a cylindrical surface at speed, on finished stainless steel, while also handling brass and copper components on the same line, required a solution that could manage both the curvature and the material variety without sacrificing quality or cycle time.
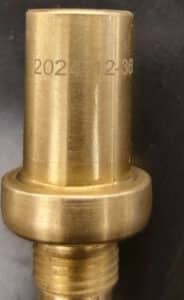
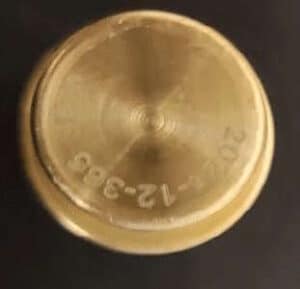
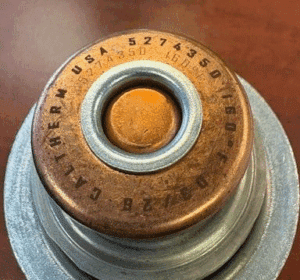
The valve bodies are small cylindrical parts. Marking on a curved surface with a flat-field laser setup means the focal point drifts as the geometry curves away, producing uneven or illegible characters. For this type of part, a rotary axis is necessary to mark the entire surface of the part
The production line processes three materials: stainless steel, brass, and copper. Each absorbs laser energy differently, so SIC MARKING had to define and deliver adapted marking parameters for each material to ensure consistent mark quality across the full range of parts.
The process runs manually, with a single operator per shift across three shifts. The setup had to be straightforward enough to produce repeatable results regardless of the operator on station.
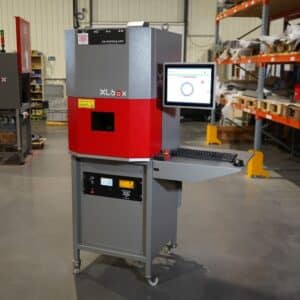
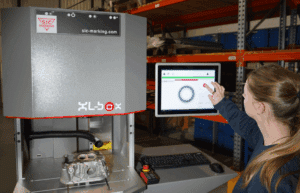
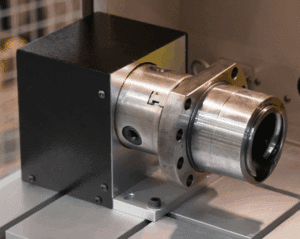
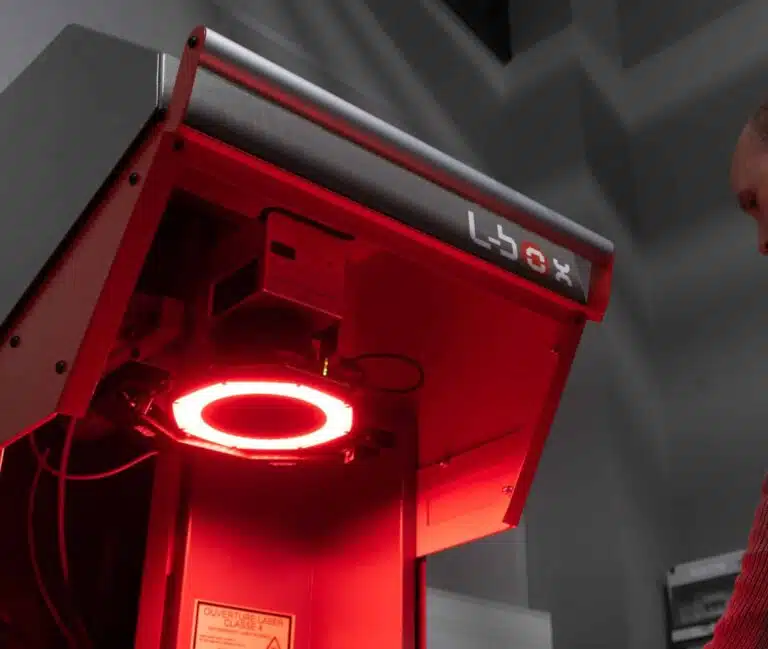
SIC MARKING recommended the XL Box EASY equipped with a 30W fiber laser source, combined with a rotary axis, a dedicated chassis fixture, and a 254 mm focal length lens. A Fumex extraction unit was integrated to maintain air quality in the clean production environment.
The 30W source was selected specifically to meet the 5-second cycle time requirement.
The rotary axis allows the system to mark around the full circumference of the valve body.
The 254 mm lens provides a working field suited to the small part dimensions and the required character size for readable alphanumeric content. The entire configuration is standard equipment, assembled from SIC MARKING’s existing product range and adapted to customer’s fixturing needs without requiring custom engineering.
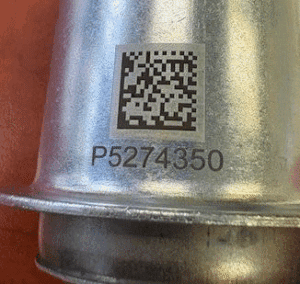
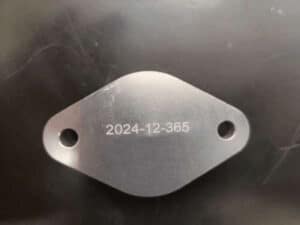
The system achieved the target cycle time of 5 seconds per part from the initial production runs. Mark quality met readability requirements for serial numbers, staging numbers, and company identification, on stainless steel valve bodies as well as on brass and copper components.
SIC MARKING provided the marking files and adapted laser parameters for each material, so that the customer could start production with a validated setup rather than spending time developing parameters in-house.
Each part now carries a permanent identification that supports both in-house tracking of manufacturing defects and external traceability throughout the product lifecycle. The standard configuration, operated manually across three shifts, delivers repeatable results without operator-dependent adjustments. Sample marking reports and part photographs documented during qualification confirmed that the mark quality and production rate meet the defined specifications.